Tag: Galvanizing Furnace
When a hot dip galvanizing plant is being planned, fuel selection usually gets settled in a single meeting – often on the basis of what is available at the site boundary. Then it quietly governs the plant’s economics for the next fifteen to twenty years.
The furnace is where the largest share of a galvanizing plant’s energy bill is generated. It has to hold a kettle full of molten zinc at roughly 445-455°C, every hour the plant runs, and it has to do so without creating hot spots on the kettle wall. Which fuel you burn to do that decides your cost per tonne, your emission compliance position, and to a real extent how long your kettle lasts.
Here is how the four practical options compare, and how to work out which one actually suits your plant.
What the Furnace Is Really Being Asked to Do
Before comparing fuels it helps to be clear about the heat load. A galvanizing furnace has two distinct jobs. The first is melt-down: taking a solid zinc charge to working temperature after a shutdown, which is a large, one-time heat input. The second, and the one that dominates your fuel bill, is holding: replacing the heat continuously lost through the kettle walls, the bath surface, the furnace lining and the work being dipped into it.
Holding load is where furnace design earns its money. A well-insulated shell lined with high-density ceramic fibre, combined with burners that can turn down accurately, will consume dramatically less fuel than an older refractory-brick furnace running continuously modulating burners – regardless of which fuel is in the pipe. That is the logic behind pulse fired high velocity burner technology, which fires in controlled pulses at near-optimum efficiency instead of throttling down into an inefficient flame.
The Four Options Compared
Natural gas (PNG or LNG)
Where a piped natural gas connection is available, it is usually the strongest all-round choice. It burns clean, needs no on-site fuel storage, no handling labour and no filtration, and it gives precise, repeatable burner control – which translates directly into tighter bath temperature and gentler treatment of the kettle. Emission-wise it is the easiest fuel to defend before a pollution control board.
The limitation is availability. PNG depends on a pipeline reaching your industrial estate, and tariffs are set by the local gas distributor rather than by an open market. Where no pipeline exists, LNG delivered and regasified on site is an option, but it brings back the storage infrastructure that piped gas avoids.
LPG
LPG is the practical answer for plants located away from a gas grid. It has a high calorific value per kilogram, burns almost as cleanly as natural gas, and gives you the same quality of burner control. Many plants run on LPG for years and switch to PNG only when a pipeline finally arrives.
Diesel, LDO or furnace oil
Oil firing remains common, particularly in older plants and in locations with neither pipeline gas nor convenient LPG logistics. Fuel is available anywhere by tanker, storage is straightforward, and the technology is thoroughly proven.
The drawbacks accumulate over time. Oil firing needs heating, filtration and atomisation, so there is more to maintain. Combustion is less clean, which means more frequent stack monitoring and a harder conversation as state emission norms tighten – several regions have already restricted the dirtier oil grades for industrial heating. Diesel and LDO are also exposed to market price volatility in a way that contracted gas usually is not. Oil-fired systems can absolutely be run well, but they demand more attention to hold the same bath temperature band.
Side-by-Side Comparison
| Parameter | Natural Gas (PNG) | LPG | Diesel / LDO / FO |
| Indicative calorific value | ~8,500–9,500 kcal/SCM | ~11,000–11,900 kcal/kg | ~9,800–10,500 kcal/kg |
| On-site fuel storage | Not required | Bottles | Tank + heating & filtration |
| Burner / heat control | Excellent | Excellent | Good, needs upkeep |
| Emissions position | Cleanest combustion | Very clean | Highest scrutiny |
| Melt-down speed | Fast | Fast | Fast |
| Maintenance load | Low | Low–moderate | Highest |
| Best suited to | Plants on a gas pipeline | Plants off the gas grid | Remote sites, existing oil plants |
Calorific values are indicative and vary by supplier and grade. Use your own supply contract figures when you run the numbers below.
How to Calculate Your Real Running Cost Per Tonne
Comparing fuels on their headline rate – rupees per kilogram against rupees per SCM against rupees per unit – tells you nothing, because you are comparing different quantities of heat. Convert everything to cost per unit of useful heat instead:
Fuel required per hour = Furnace heat load (kcal/h) ÷ ( Calorific value × Furnace efficiency )
Then multiply by your delivered fuel rate, and divide by tonnes galvanized per hour. Three things decide whether the answer is honest:
- Delivered rate – use your delivered price, including transport, taxes, demand charges and any regasification or handling cost – not the ex-terminal rate
- Efficiency – this is where furnace design shows up. A modern pulse fired, ceramic-fibre-lined furnace and a tired brick-lined one burning the same fuel can differ enormously in fuel consumed per tonne
- Real operating pattern – include holding hours during breaks, weekends and shutdowns, not just productive dipping hours – many plants are surprised by how much of the annual bill is idle holding
Run that calculation for each fuel you can realistically obtain, and add the capital cost of the associated infrastructure amortised over the plant life. This is the same exercise that sits behind any serious costing of a galvanizing plant and its technology.
Four Factors That Override the Fuel Rate
- Supply security – A cheaper fuel you cannot get reliably is not cheaper. Confirm pipeline pressure and committed volume, or tanker logistics to your location, before deciding.
- Emission regulation – State norms are moving in one direction. A fuel that clears today may need abatement or substitution within the plant’s life, and retrofitting later costs more than choosing correctly now.
- Kettle life – Uniform heat around the kettle wall matters more than which fuel produces it. Hot spots shorten kettle life, and a replacement kettle plus the lost production is an expense that dwarfs any fuel saving.
- Statutory approvals – LPG storage installations and gas connections carry approval, safety-distance and periodic inspection obligations that oil storage does not, and vice versa. Budget the effort, not just the equipment.
Kettle protection deserves particular weight in this decision. Sizing and heating are closely linked, and it is worth reading how to match kettle size to production requirement alongside this fuel comparison.
So Which One Should You Choose?
For most new plants in India the decision resolves quickly. If a piped natural gas connection is available and the committed volume is adequate, take it. If it is not, LPG is the next best choice and keeps you on clean, precisely controllable combustion. Oil firing makes sense where neither is practical or where an existing oil-fired plant is running well and a full conversion cannot yet be justified. Electric heating is a niche answer for small kettles and job-work operations.
Where gas supply is new or unproven, a dual-fuel furnace – gas with oil as fallback – removes the single biggest operational risk, because a kettle that freezes during an extended supply interruption can be damaged beyond repair. The comparatively modest additional cost buys continuity.
Frequently Asked Questions
- Can an existing diesel-fired galvanizing furnace be converted to natural gas or LPG?
Yes, in most cases. The furnace shell, ceramic fibre lining and kettle support structure are usually retained, while the burners, fuel train, combustion air arrangement and burner management system are replaced. Conversion is far cheaper than a new furnace and is commonly done when a PNG pipeline reaches an industrial estate. Have the existing shell and lining condition surveyed first, because a conversion on a furnace nearing the end of its life is money spent twice.
- Does fuel choice affect zinc consumption and dross generation?
Indirectly, and significantly. Zinc consumption is driven by bath temperature stability rather than by the fuel itself. Any fuel and burner combination that produces hot spots on the kettle wall raises local zinc temperature and accelerates dross and zinc ash formation. Gaseous fuels with pulse fired high velocity burners hold a tighter temperature band than older oil-fired systems with continuously modulating burners, which is why they typically show lower zinc loss per tonne.
- Is a dual-fuel galvanizing furnace worth the extra cost?
It is worth it wherever gas supply is new, seasonal or subject to interruption. The additional cost sits mainly in the second fuel train and burner arrangement, and what it buys is continuity – a galvanizing kettle that is allowed to freeze can be damaged beyond repair. Plants on an established pipeline with no history of interruption often skip it.
- Which fuel melts the zinc bath fastest after a long shutdown?
High-output gaseous and oil-fired burners bring a bath up faster than electric resistance heating, because they deliver a far higher heat input per hour. Speed is not the objective, though. Melt-down has to follow a controlled ramp so that the solid zinc expands evenly and does not stress the kettle walls, so a controllable burner system matters more than raw firing capacity.
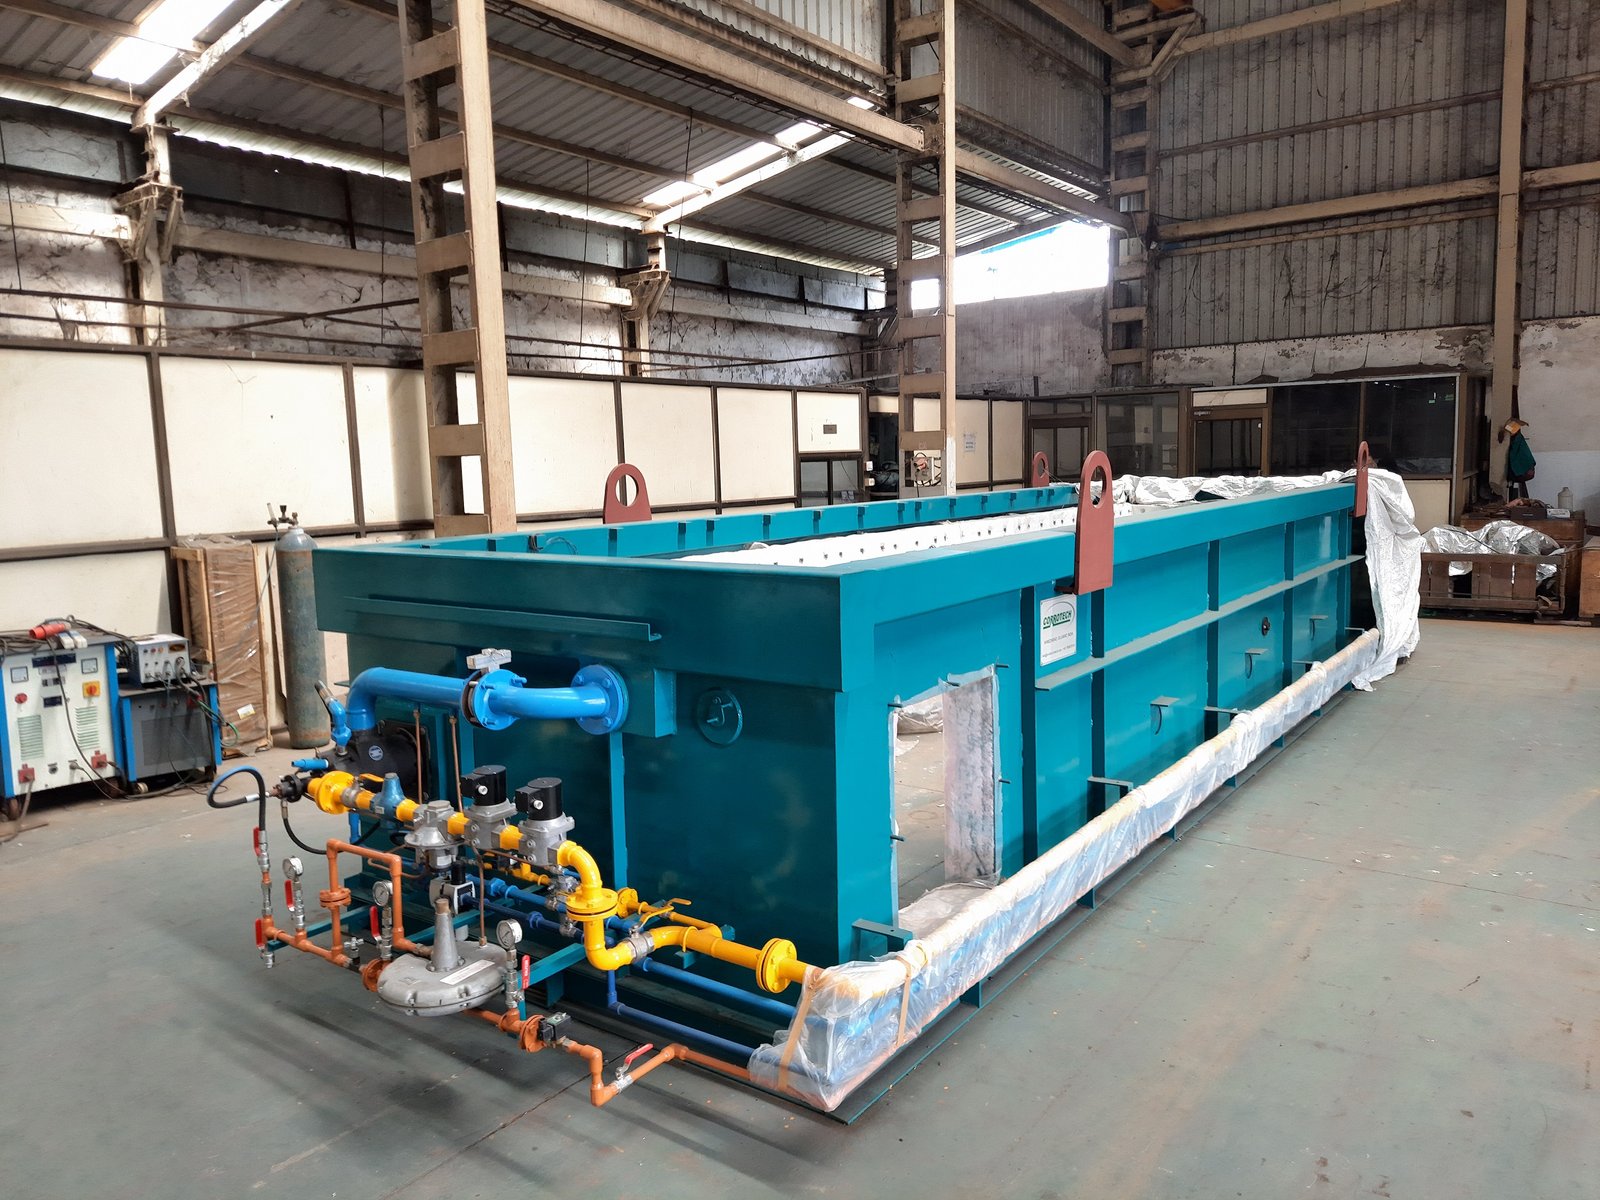
Scientists and socio-economic experts tracking the evolution of technology and innovation, and their impact on development have rightly called the invention of Galvanizing Furnace a milestone. The emergence of Galvanizing furnace has transformed the industry, especially the galvanizing sector.
So, what do you understand about the revolutionary product? What comes to your mind when you hear about product? Directly or indirectly, we all come across galvanized products. It could be a car, an auto rickshaw, an airplane, telecommunication and a wide range of construction material. However, we hardly ponder over the Galvanizing Furnace Process.
This blog makes a humble attempt to expand the knowledge of the readers about the landmark product.
Understanding the product
The Galvanizing Furnace is a sophisticated enclosure machine wherein the material is heated at a high temperature. A technology-driven temperature management system continuously keeps tabs on the temperature. The shelf life of this industry-centric product varies from company to company. Generally, it’s 20 years.
Whereas the requisite thermal energy is produced inside the combustion chambers during the galvanizing furnace process, the reason being, to keep the molten zinc according to the optimal temperature range. Heating intensity within the enclosure depends on the fuel being used. Fuels like gas, oil and electricity are being used. How to achieve excellence in a combustion chamber? That’s a moot question often raised by industry owners. Well, in this era of technology, flaws and excellence can be easily measured. Achieving excellence in combustion chamber remains the top priority of the industries. It’s the end result of accurate energy, balance calculation, construction engineering, quality of the enclosure and insulation material.
A kettle containing zinc gets heated through the Galvanizing Furnace. As far as the life of the kettle is concerned–it’s 7 – 9 years.
Industry experts recommend flawless fabrication technique to achieve brilliant quality hot dip galvanized coatings on fabricated article. Make sure that the fabricated assemblies, castings and other tools and technology for the Galvanizing Furnace Process conform to the local and global standards.
Heart matters
The industry experts weren’t exaggerating when they called the galvanizing furnace as the heart of a hot dip galvanizing plant. Engineering and design are important. Features like energy efficiency, durability and quality among others depend on design and engineering of the furnace. It doesn’t end here; even the profitability and performance of the furnace depend on engineering.
Ultimately, even the profitability of the plant is deeply connected to the quality of furnace engineering
Material used in manufacturing the kettle
The Galvanizing Kettle is manufactured using the special steel material with low carbon and silicon contents. The product has the strength to overcome the collision of zinc, and can endure high temperature.
Advantages of galvanization
Research has proved that galvanization is the best process to provide coating for metal and steel. A galvanized coating is unique in the sense that it’s an alloy of steel and matches features of steel.
Galvanization has been a blessing in disguise for the economic development. Here are a few advantages of galvanization:
- Lowest first cost
- Lowest long term cost
- Increases durability of the steel
- Reliability
- Robust coating
- Automatic protection for damaged areas
- Complete protection
- Entire surface can be coated within no time.
There are several types of coatings available to protect steel from corrosion. However, none of the coating matches benefits and properties of galvanization.
I’m confident, the blog will expand your knowledge base!
Leverage the unique expertise of Arvind Corrotech Ltd.
Arvind Corrotech is one of the leading companies offering Hot Dip Galvanizing Plants, Pulse Fired High Velocity furnaces, Pickling Tank, Flux Tank, Rinse Tank, Fume Extraction System, material handling systems and a wide range industrial storage tanks. The niche created through excellence enable the manufacturer with headquarter in Ahmadabad, India to cater to global companies.